English
 Español
 عربى
Home / News / Industry News / RF Defrosting vs. Microwave Defrosting: The Battle of Efficiency and Quality in Industrial Production of Large Meat Blocks


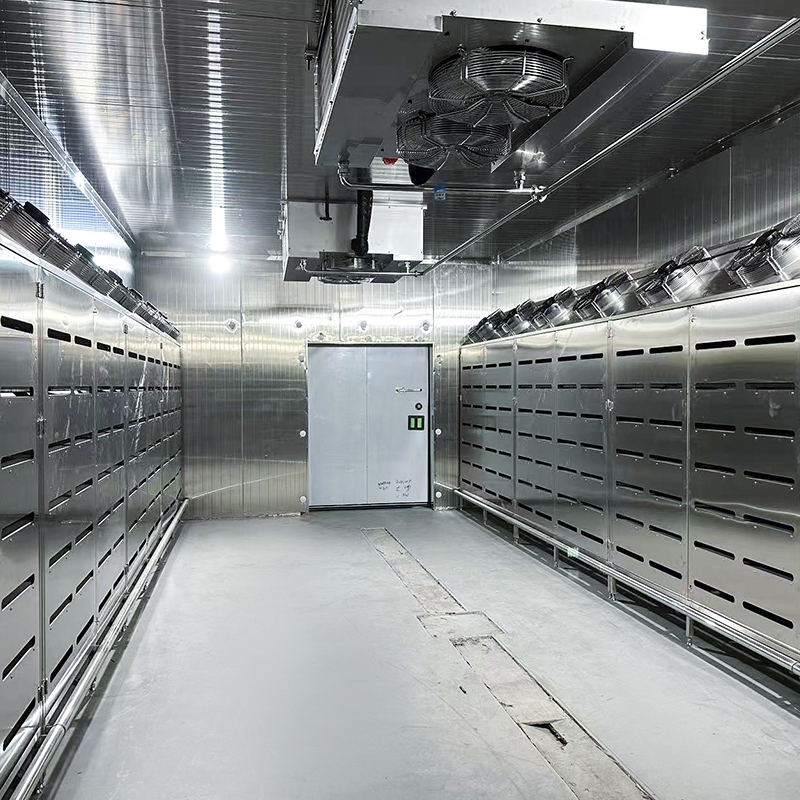
Large frozen meat blocks are unforgiving. A 25 kg block of lean beef can take days to thaw in air, hours in water, and yet only minutes in an electromagnetic field. That is why technical decision makers at meat processing plants are increasingly comparing meat defrosting equipment built on two rival platforms: radio frequency (RF) and microwave. Both heat volumetrically. Both slash thawing time. But when the product is thick, dense, and irregularly shaped, the physics diverge sharply and the operational consequences compound.
This article does not recycle generic definitions. It examines penetration depth, thermal uniformity, drip loss, protein integrity, throughput, and total cost of ownership through the lens of large meat block production. The goal is practical: help you determine whether RF or microwave meat defrosting equipment matches your line reality.
A large frozen meat block is not simply a scaled-up steak. It is a thermal challenge with three simultaneous constraints.
Not every meat defrosting equipment platform handles these constraints equally. Air thawing is too slow. Water immersion creates wastewater and hygiene risk. Vacuum thawing is batch-limited. High-voltage electrostatic thawing remains niche. RF and microwave dominate the industrial conversation because both can thaw a 20 kg block in under 30 minutes under controlled conditions. The question is which one does it without damaging the product.
Industrial reality: A 25 kg frozen beef block at -18 C requires approximately 4,200 kJ to reach -1 C. Delivering that energy uniformly is the engineering problem that separates RF from microwave.
Both technologies use electromagnetic waves to excite polar molecules inside the food. The frequency determines how deeply those waves penetrate and how the energy distributes.
Penetration depth is the distance at which electromagnetic power drops to roughly 37 percent of its surface value. In frozen meat, this depth is inversely related to frequency. RF at 27.12 MHz penetrates several times deeper than microwave at 915 MHz, and dramatically deeper than 2450 MHz.
Patent literature and peer-reviewed studies consistently state that microwave penetration is insufficient for large packaged food blocks. RF dielectric heating, by contrast, provides adequate penetration for thick frozen meat, even when the product is irregularly shaped or densely packed.
For a 15 cm thick frozen block, microwave energy at 2450 MHz may be largely absorbed within the outer 2 to 3 cm. The core then thaws by conduction, creating the very temperature gradient the technology was meant to eliminate. RF meat defrosting equipment does not suffer this limitation to the same degree.
Speed alone is a misleading metric. A microwave unit can thaw a thin patty in seconds. But for a 20 kg meat block, speed without uniformity produces partial cooking, drip loss, and rework.
Industrial RF meat defrosting equipment typically processes 500 kg to 2,000 kg per hour in continuous tunnel configurations. Microwave batch systems may claim similar peak throughput, but effective throughput drops when blocks require tempering, rotation, or additional holding time to equalize internal temperatures.
Comparative studies on RF versus microwave heating of frozen meat consistently report that RF achieves a narrower temperature distribution. Microwave heating shows a statistically significant center-to-corner temperature difference, often exceeding 15 C in large blocks. That gradient means the surface may reach 40 C while the core remains at -5 C.
Thermal runaway: In microwave thawing, once ice converts to liquid water, the dielectric loss factor increases by an order of magnitude. Water heats faster than ice. The already-thawed surface absorbs more energy, while the frozen core receives less. RF reduces this risk because its deeper penetration maintains a more balanced field across the block.
Quality is where the economic argument becomes concrete. Drip loss is not a cosmetic issue. It is lost yield, lost revenue, and often lost customer satisfaction.
The economic translation is straightforward. For every 100 tonnes of raw material thawed, a 1 percent reduction in drip loss recovers 1 tonne of saleable product. At industrial volumes, that single percentage point often justifies the higher capital cost of RF meat defrosting equipment within the first year of operation.
RF heating also avoids the surface-to-core conduction dependency that damages cell structure. Because energy is deposited throughout the volume, muscle fibers thaw more gently and hold more of their natural moisture.
Selection is not about declaring a universal winner. It is about matching technology to product, throughput, and quality tolerance.
Industrial RF defrosting systems generally carry a higher purchase price than microwave alternatives. However, the relevant comparison is not sticker price. It is cost per tonne of correctly thawed product.
RF is generally better suited for large frozen meat blocks because its longer wavelength penetrates deeper and produces a more uniform temperature distribution. Microwave energy at common industrial frequencies is absorbed closer to the surface, which can leave the core frozen while edges begin to cook.
Continuous RF thawing tunnels commonly process between 500 kg and 2,000 kg per hour, depending on block size, starting temperature, and target end temperature. Batch cabinets handle smaller volumes but offer flexibility for mixed product loads.
RF energy heats the entire volume of the product simultaneously rather than relying on surface heat conduction. This avoids localized overheating that ruptures cell membranes. When cells remain intact, they retain their natural moisture, and drip loss is minimized.
Microwave batch thawing units may start around 16,000 USD for small capacities. RF systems carry a higher initial investment, often ranging from 200,000 USD to over 1,000,000 USD depending on throughput and automation level. The relevant metric is cost per tonne of correctly thawed product, where RF often achieves lower long-term cost through yield recovery.
Yes. RF thawing works effectively with both packaged and unpackaged products, including vacuum-sealed blocks, cardboard cartons, and plastic-lined combos. The electromagnetic field penetrates common packaging materials without heating them significantly.
For large frozen meat blocks, RF meat defrosting equipment demonstrates clear advantages in penetration depth, thermal uniformity, and drip loss control. Microwave systems retain value for thinner products, lower throughput requirements, and budget-constrained operations where some yield loss is acceptable.
The decision should be driven by product geometry, quality standards, annual volume, and the true cost of moisture loss. A technology demonstration or sample test on your actual product provides the most reliable data for selection.
To discuss your specific application and request a performance estimate, contact our engineering team for a no-obligation consultation.
Introduction: The New Era of Food Defrosting Technology The global demand for frozen food products h......
READ MOREIntroduction to Advanced Food Preservation The evolution of food preservation technology has reached......
READ MOREIntroduction: What Is a Tunnel Freezer? A Tunnel Freezer is a specialized industrial freezing system......
READ MORE1. Introduction In the context of the global food processing industry's continuous growth, food safe......
READ MOREDevelopment Concept
Guided by our core principle of quality, we have always adhered to the business purpose of "starting with pursuit and ending with satisfaction.
 +86-13967365006
 +86-573-82723906
 zhejiangkanglian@gmail.com
 No. 351 Xinfei Road, Fengqiao Town Industrial Park, Nanhu District, Jiaxing City, Zhejiang Province, China
Copyright © 2023 Zhejiang Kanglian Intelligent Equipment Co., Ltd. All Rights Reserved. Privacy Global Technical Support for Custom Food Processing Equipment